LFP Battery Pack Procurement Checklist for Cycle Life, Safety, and Warranty
LFP Battery Pack Procurement Checklist for Cycle Life, Safety, and Warranty
Selecting an LFP Battery Pack is rarely a simple capacity-and-price exercise. That becomes especially clear when the battery will power off-road machinery, articulated boom lifts, or a stationary energy storage system expected to operate every day. A lower quotation can look attractive at purchase order stage, then become expensive through reduced runtime, inconvenient charging, premature replacement, service delays, or warranty exclusions that only become visible after a fault occurs.
Lithium iron phosphate chemistry is widely considered a practical choice where long service life and a stable thermal profile matter. Still, “LFP” is only the chemistry label. It says very little by itself about cell consistency, pack engineering, battery management logic, enclosure protection, charging compatibility, or the supplier’s willingness and ability to support the product after delivery. Procurement decisions should therefore move from buying a rated kWh figure to buying a usable, supportable power system.
The most reliable way to compare suppliers is to ask the same technical and commercial questions of each one, then judge the answers against the actual duty cycle. A warehouse boom lift, for example, faces a different electrical and environmental profile from a grid-connected storage cabinet. Treating them as equivalent often produces a battery that works on paper but creates operational friction in the field.
Start With the Load Profile, Not the Nameplate Capacity
A procurement brief should state more than nominal voltage and required energy. Ask the equipment team for peak discharge current, average current, operating hours, expected charging window, ambient temperature range, slope or vibration exposure, and whether the battery must communicate with the vehicle controller or charger. These details determine whether a proposed LFP Battery Pack is genuinely matched to the application.
A common mistake is to compare two packs only by nominal capacity. A pack with more amp-hours may still be the weaker option if its continuous discharge capability, low-temperature charge limits, or voltage range does not align with the machine. Conversely, specifying excessive capacity can add unnecessary mass and cost, particularly in mobile equipment where weight affects transport, stability, and usable payload.
For a 51.2V platform, confirm the full operating range rather than assuming the nominal voltage tells the whole story. The host equipment, charger, contactors, DC/DC converter, and onboard controls must tolerate the pack’s actual upper and lower voltage limits. This is a commissioning issue as much as a purchasing issue. A mismatch discovered after several units arrive is far more difficult to resolve than one found during technical evaluation.
Questions that expose a weak specification
- What are the required continuous and peak charge/discharge currents, and for how long do peaks occur?
- Is the quoted capacity nominal, usable, or guaranteed at a specified discharge rate and temperature?
- What voltage thresholds trigger warning, derating, disconnect, and recovery?
- Will the application operate in cold, dusty, wet, high-vibration, or high-altitude conditions?
- Does the pack need CAN communication, a specific connector, emergency stop interface, or charger handshake?
- Can the supplier provide a dimensional drawing, mass, mounting requirements, and service access arrangement before order release?
If a supplier answers these questions only with a brochure, the design is probably not ready for a serious equipment program. The useful response includes limits, assumptions, interface information, and a clear indication of what still needs validation on the customer’s machine.
Evaluate Cycle Life as a System Claim
Cycle life is often the first figure buyers ask for and one of the easiest figures to misunderstand. It depends on depth of discharge, charge and discharge rate, cell temperature, charge cutoff, storage conditions, and the definition of end-of-life capacity. Two suppliers may both describe a pack as “long cycle life” while testing at entirely different conditions.
Request the cycle-life test conditions, not merely the cycle count. Useful documentation identifies the charge method, discharge rate, temperature, depth of discharge, rest periods if applicable, and residual-capacity criterion. It should also distinguish cell-level data from battery-pack expectations. A well-made pack can protect cells through balanced operation and sensible thermal design, but pack life is also affected by contactors, fuses, harnesses, BMS calibration, and mechanical installation.
For equipment with irregular shifts, calendar aging deserves attention alongside cycling. A battery that spends long periods at a high state of charge in a hot enclosure may age differently from one used daily and recharged promptly. Procurement teams should describe the expected idle periods and seasonal storage pattern. This is not an academic detail; it influences both operating guidance and the warranty conditions that are reasonable for the project.
Do not assume that a higher permissible C-rate is automatically better. High-rate capability can be valuable where hydraulic loads or drive systems create sharp current demand, but it may not justify a premium in a low-power stationary application. The better question is whether the pack’s rating gives enough margin for the measured load profile without persistent heat buildup or nuisance protection events.
Safety Review: Look Beyond the Chemistry
LFP chemistry is often selected for its thermal stability relative to some other lithium-ion chemistries, but safe deployment still depends on the entire battery system. The procurement file should cover electrical protection, mechanical protection, software controls, transport handling, and installation conditions. A safe cell in an inadequately protected pack is not a safe field solution.
Review the battery management system in practical terms. It should monitor relevant cell and pack conditions, manage charge and discharge permissions, and respond predictably to abnormal voltage, current, or temperature conditions. Ask what fault information is available to the machine operator, service technician, or remote monitoring platform. An unexplained shutdown can become an expensive maintenance event when no usable diagnostic record is available.
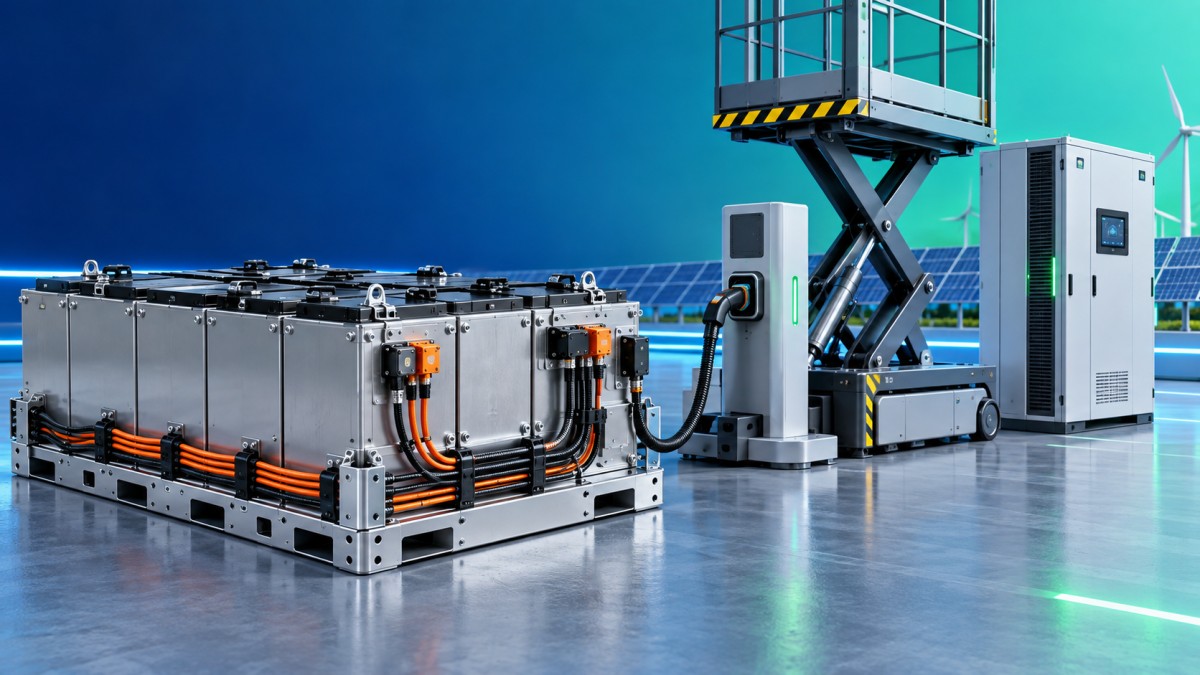
For off-road machinery, enclosure design deserves the same attention as electrical performance. Check ingress protection requirements for the intended location, mounting points, cable strain relief, connector selection, vibration considerations, access to service disconnects, and the consequences of a damaged enclosure. Natural cooling can be appropriate when the duty cycle and installation provide adequate thermal margin, but it must be assessed against ambient heat, restricted airflow, and repeated high-current operation.
Compliance requests should be specific to the sales market and application. Buyers commonly need to verify transport documentation such as UN 38.3 where applicable, while stationary or industrial use may involve other relevant product, installation, or local regulatory requirements. Do not use a generic certificate list as a substitute for review. Ask which documents apply to the exact pack configuration, destination, and intended use, and obtain copies early enough for the project team to check them.
Check Consistency Before Scaling an Order
A prototype that performs well is encouraging, but repeatability is the real procurement concern. In a fleet or storage project, variation between packs can complicate charger settings, runtime expectations, fault diagnosis, and spare-parts planning. Ask how incoming cells are inspected, matched, traced, and controlled through pack assembly. The supplier does not need to disclose every manufacturing detail, but should be able to explain its traceability approach and change-control process.
This matters when components change. A different cell source, BMS revision, connector, fuse, or enclosure detail may affect performance or compatibility. Put notification requirements in the supply agreement: which changes require customer approval, which require updated drawings or test evidence, and how existing equipment will be supported if a revision is introduced. Without this discipline, two products carrying the same model name can gradually become different products.
A practical pre-shipment plan can include visual inspection, verification of labels and serial numbers, voltage and functional checks, communication checks, and confirmation that the agreed charger interface is present. The exact acceptance test should be proportionate to order size and project risk. For a first deployment, a pilot batch or sample integration is usually more informative than a long spreadsheet comparison.
Read the Warranty Like an Operating Manual
Warranty length is a poor comparison point unless its triggers and remedies are understood. Some warranty language is tied to time, some to cycle count, some to remaining capacity, and some to strict operating conditions. The buyer needs to know what happens when a pack loses usable capacity, stops communicating, develops an internal fault, or repeatedly enters protection during normal operation.
Ask for the warranty document before contracting, then clarify these points:
- What measurable condition qualifies as a warranty claim?
- Which operating limits, charging methods, storage conditions, and installation practices are mandatory?
- Is diagnosis remote, onsite, or performed after the pack is returned?
- Who bears freight, labor, removal, installation, and customs costs where relevant?
- Will the remedy be repair, replacement, credit, or another arrangement?
- What is the expected availability of spares, technical documents, firmware support, and service contacts?
Pay close attention to capacity warranties. Capacity fade is gradual, whereas many field problems are caused by communication errors, contactor failures, charging incompatibility, or a BMS fault. A warranty focused only on cell capacity may leave important pack-level risks outside the remedy. The commercial team should also consider response time. For equipment that generates revenue only when operating, a quick technical diagnosis can matter as much as the replacement cost of the battery itself.
Use Configuration Details to Compare Real Value
The right configuration should make daily operation easier, not simply raise the specification sheet numbers. Consider an articulated boom lift application: a 51.2V battery family may be offered in capacities from 230Ah to 460Ah, corresponding to stated total energy options from 11.776kWh to 23.552kWh. That range creates useful choice, but only after runtime, vehicle mass, charging schedule, and available installation volume are understood.
For example, the Articulated Boom Lift Battery Pack range includes 1P16S, 2P16S, and 4P16S configurations, a 40–58.4V working range, natural cooling, and AC or AC+DC charging options. Its maximum continuous charge/discharge rating is stated as 1C at 25℃. Those are meaningful starting points for engineering review, not automatic proof of fit. A buyer should still verify charge infrastructure, actual ambient conditions, peak-load behavior, physical integration, and the control-system interface.
This is where a supplier with application knowledge is more useful than one that only trades cells or standard packs. EN New Power Technology (Shandong) Co., Ltd., established in 2020 as a wholly-owned subsidiary of a listed company, works across R&D, manufacturing, and sales for off-road machinery power systems and smart-grid energy storage solutions. For buyers, the practical value of that type of integrated capability is the ability to discuss pack design, manufacturing control, and after-sales responsibility without handing a problem between unrelated parties. That said, each project still needs its own technical validation.
Build the Decision Around Total Cost of Ownership
The cheapest LFP Battery Pack is not necessarily the lowest-cost purchase once commissioning, charging equipment, downtime exposure, service labor, and replacement timing are considered. Equally, the most expensive offer is not automatically safer or longer-lived. The useful comparison is a documented one: price, usable energy, interface scope, validation work, expected service process, warranty remedy, delivery lead time, and change-control commitments.
Before placing a production order, ask the supplier to confirm the final configuration in writing: model, voltage range, capacity, current limits, cooling approach, charging method, communication protocol, connector arrangement, dimensions, labeling, documentation, and warranty version. Keep this approved configuration linked to the purchase order. It protects both sides when replacement packs or later production batches are required.
Good battery procurement is not about extracting the lowest unit price from a generic quotation. It is about removing the costly uncertainties that appear after the battery reaches the machine or site. When cycle-life assumptions, safety controls, production consistency, and warranty responsibilities are examined before award, the final decision is usually clearer—and considerably easier to defend when the equipment is in service.